
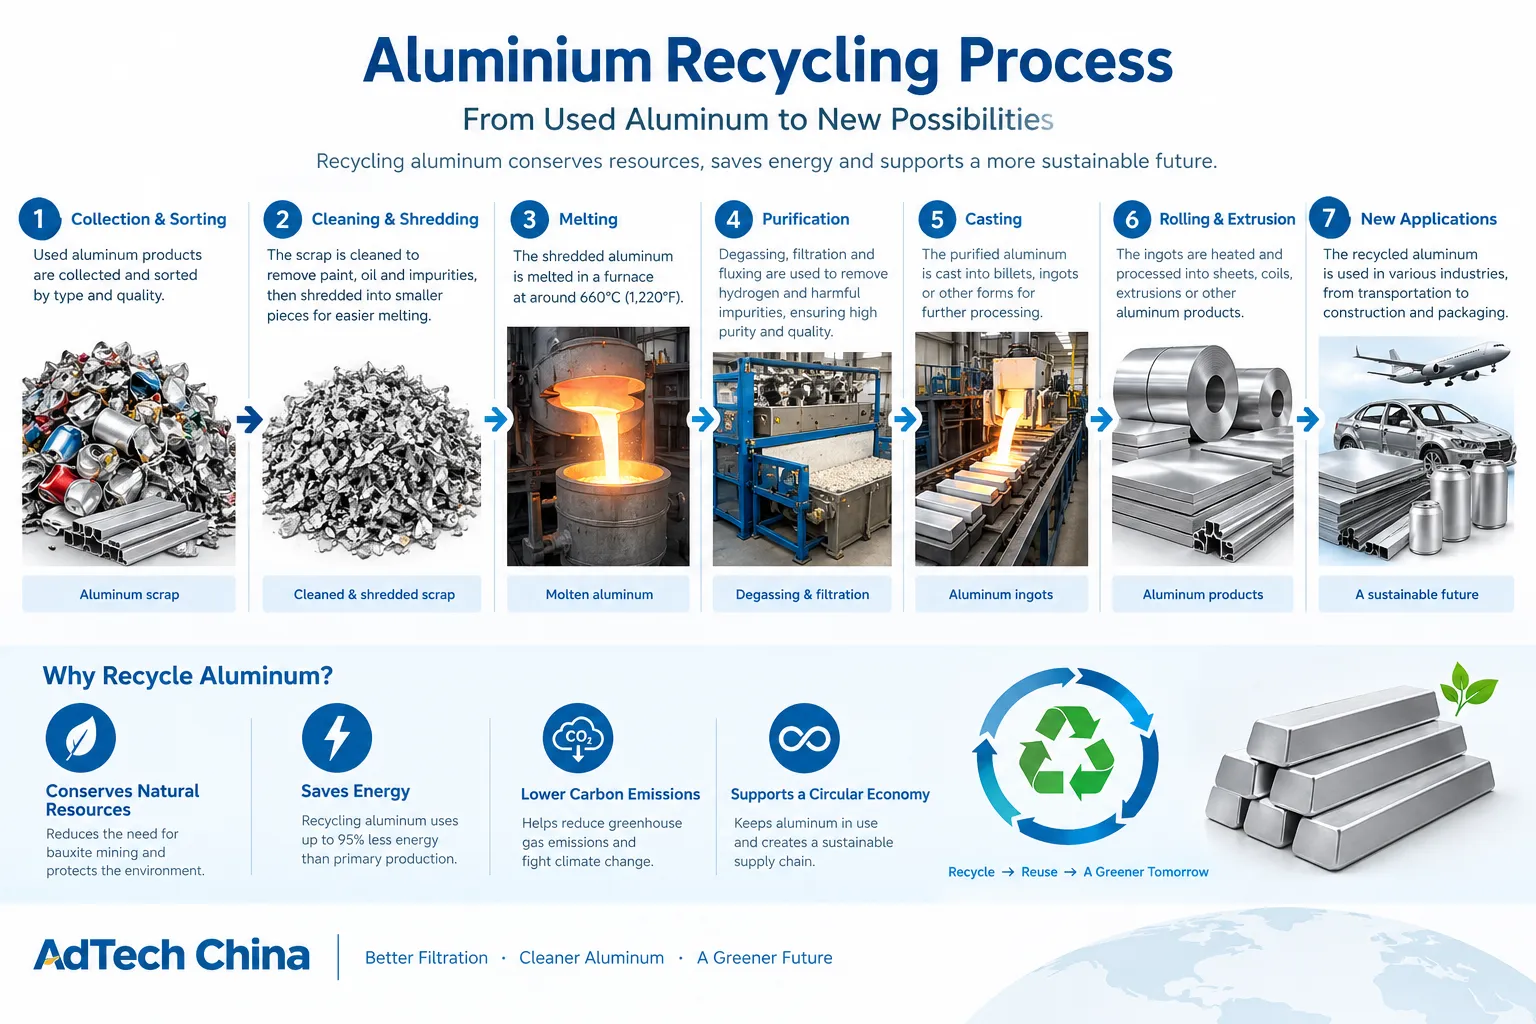
The aluminium recycling process converts aluminium scrap into reusable metal through collection, sorting, pre-treatment, melting, melt refining, alloy adjustment and casting. The exact process depends on the scrap source, alloy composition, contamination, coating, moisture content and the quality required for the final product. For industrial recyclers, the objective is not simply to melt aluminium, but to recover as much usable metal as practical while controlling alloy chemistry, inclusions, hydrogen, emissions and production costs.
Aluminium recycling is widely used to produce secondary aluminium for foundry alloys, extrusion billets, rolling slabs and other applications. Compared with producing primary aluminium from bauxite, recycling generally requires substantially less energy. However, achieving consistent recycled metal quality requires suitable scrap preparation and process control.
1. Aluminium Recycling Process at a Glance
The following table summarizes the main stages of industrial aluminium recycling.
| Stage | Main operation | Primary objective |
|---|---|---|
| 1. Collection | Gather manufacturing scrap and end-of-life aluminium | Establish a usable feedstock supply |
| 2. Sorting | Separate aluminium from other materials and classify scrap | Improve alloy consistency and reduce contamination |
| 3. Pre-treatment | Shred, size, dry, de-oil or remove coatings as required | Prepare scrap for safe and efficient melting |
| 4. Melting | Charge scrap into a suitable furnace | Convert solid aluminium into molten metal |
| 5. Fluxing and skimming | Apply suitable flux where required and remove surface residues | Control oxidation, separate residues and recover metal |
| 6. Melt refining | Adjust chemistry and remove unwanted melt constituents | Meet the target alloy and melt-quality requirements |
| 7. Degassing and filtration | Remove dissolved hydrogen and non-metallic inclusions when necessary | Improve melt cleanliness |
| 8. Casting | Produce ingots, billets, slabs or other cast forms | Prepare the metal for downstream manufacturing |
| 9. Quality control | Analyze composition and verify relevant quality properties | Confirm suitability for the intended application |
These stages are not identical in every recycling facility. Clean manufacturing scrap may require relatively little preparation, while mixed post-consumer scrap may require several separation and treatment steps before melting. Some facilities combine melting and refining operations, while others transfer molten metal between separate furnaces or treatment stations.
2. Collection and Classification of Aluminium Scrap
The recycling process begins with identifying where the scrap comes from and what it contains.
Manufacturing scrap
Manufacturing scrap is generated during the production of aluminium products. Examples include sheet offcuts, extrusion remnants, machining chips and foundry scrap.
Clean, segregated manufacturing scrap can often be recycled efficiently because its origin and material characteristics are relatively well known. However, oily chips, mixed alloys and materials containing coatings may need additional treatment.
Post-consumer aluminium scrap
Post-consumer scrap comes from products that have reached the end of their useful life. Common examples include:
-
Used aluminium beverage cans and packaging.
-
Aluminium window frames and building components.
-
Vehicle components.
-
Household and industrial aluminium products.
-
Mixed aluminium components containing steel, plastics, rubber or other materials.
Post-consumer scrap generally presents a greater sorting challenge because its previous application, alloy composition and contamination level may be uncertain.
Aluminium dross and other process residues
Aluminium dross is generated during melting and metal handling. It contains aluminium oxide, other constituents and potentially recoverable metallic aluminium.
Dross should not be treated as equivalent to clean aluminium scrap. Its recovery route depends on its composition, temperature, handling history and the available recovery technology.
The important principle is that scrap classification should happen before the furnace route is selected. A facility that treats every aluminium-bearing material as interchangeable risks poor alloy control, unnecessary processing and lower metal recovery.
3. Sorting and Separation: Why Alloy Composition Matters
Sorting is one of the most important steps in secondary aluminium production because the chemical composition of the incoming scrap directly affects the final metal.
Aluminium alloys contain different proportions of elements such as silicon, magnesium, copper and manganese. These elements influence properties such as strength, corrosion resistance, formability and castability.
For example, a high-silicon casting alloy and an aluminium wrought alloy designed for rolling may have different composition requirements. Mixing them without a suitable process plan can make it more difficult to produce the intended final alloy.
Common aluminium scrap sorting methods
| Method | Purpose | Important limitation |
|---|---|---|
| Manual sorting | Remove obvious foreign materials and separate identifiable scrap categories | Depends on operator consistency and the visibility of material differences |
| Magnetic separation | Remove ferrous materials such as steel pieces | Does not separate aluminium alloy grades from one another |
| Eddy-current separation | Separate conductive non-ferrous metals from suitable waste streams | Performance depends on material size, shape, feed presentation and equipment design |
| Sensor-based sorting | Identify and separate selected material categories or alloy groups | Requires suitable sensing technology and validated sorting criteria |
| Chemical composition analysis | Check alloy composition and support material classification | A representative sample and appropriate analytical method are required |
Laser-induced breakdown spectroscopy and colour-based sorting technologies are among the methods described by the Aluminum Association for improving scrap separation. Their usefulness depends on the feedstock and the recycling objective.
What happens when different aluminium alloys are mixed?
Mixing alloys is not automatically unacceptable. Some secondary aluminium products are designed to use mixed scrap, with composition adjusted through the process.
The problem arises when the mixture cannot meet the intended specification economically or consistently.
For example, an unwanted element that remains dissolved in the melt cannot ordinarily be removed simply by passing the metal through a ceramic filter. Depending on the element and target chemistry, practical responses may include better sorting, blending with suitable metal, changing the target product or using a more specialized metallurgical process.
Therefore, sorting is not merely a waste-handling activity. It is an important form of quality control that takes place before the metal enters the furnace. Research reviews of secondary aluminium production identify scrap composition and unwanted alloying elements as persistent challenges in producing recycled alloys.
4. Pre-Treatment: Shredding, Cleaning, Drying and Decoating
The purpose of pre-treatment is to prepare scrap for the selected melting process. Not every material requires every operation.
Shredding, shearing and sizing
Large or bulky components may be cut, crushed or shredded into manageable sizes. The required size depends on the separation equipment, furnace charging arrangement and characteristics of the scrap.
Size reduction can improve material handling and support downstream separation. However, it also consumes energy and may generate dust, so the equipment should match the actual feedstock.
Removing coatings and organic contaminants
Used beverage cans, painted components and other coated scrap may require decoating or delacquering before melting.
Coatings, oil, grease, lubricants and plastic residues can contribute to emissions and complicate the melting process. Suitable pre-treatment can improve metal recovery and reduce the contaminant load entering the furnace.
The need for thermal treatment depends on the coating and material type. It should not be assumed that every aluminium component requires the same decoating method.
Drying and de-oiling aluminium turnings
Machining chips and turnings deserve special attention because they may retain cutting fluids, oil and moisture. Their shape also gives them a relatively high surface area compared with their mass.
Suitable cleaning and drying can help prepare this material for safer charging and efficient metal recovery. The treatment method must be appropriate for the contaminant and the physical form of the scrap.
Why wet scrap is a serious safety concern
Wet or moisture-contaminated scrap must not be charged into molten metal without appropriate controls. Water contacting molten metal can cause a violent explosion.
The UK’s Health and Safety Executive advises storing scrap in dry, covered areas where possible, checking materials for water contamination and drying scrap when covered storage is not available. It also emphasizes training, appropriate protective equipment and safe operating practices.
Closed containers, trapped liquids and other potentially dangerous contaminants require specific assessment under the facility’s safety procedures.
Pre-treatment should therefore be selected based on three factors: material quality, metallurgical requirements and safe furnace operation.
5. Melting: Turning Prepared Scrap into Molten Aluminium
After preparation, the scrap is charged into a suitable melting furnace.
Pure aluminium has a melting point of approximately 660°C. Commercial alloys and industrial recycling processes operate according to their respective melting ranges and process requirements, so 660°C should not be treated as a universal furnace setpoint.
The actual operating temperature depends on alloy composition, furnace technology, charge condition, required throughput and downstream casting requirements.
Choosing a melting furnace
Different furnace designs suit different forms of scrap and production requirements.
| Furnace type | General consideration | What to evaluate |
|---|---|---|
| Reverberatory furnace | Used for melting substantial quantities of aluminium scrap and other suitable feedstocks | Capacity, thermal efficiency, charge characteristics and melt handling |
| Rotary furnace | Used in some secondary aluminium operations, particularly where scrap characteristics suit rotary processing | Scrap contamination, process residues, flux requirements and recovery performance |
| Induction furnace | Provides electromagnetic heating and may suit particular melting tasks | Furnace capacity, charge characteristics, electrical infrastructure and melt cleanliness |
| Crucible furnace | Used in selected smaller-scale or specialized melting applications | Batch size, alloy range, operating flexibility and handling arrangements |
These are general selection considerations rather than a universal ranking. Furnace suitability cannot be determined from nominal capacity alone.
One important industry distinction is the feedstock and refining route. Cleaner, well-characterized scrap may be remelted through a relatively direct process, while more contaminated or mixed scrap can require more intensive refining. Terminology such as remelter and refiner varies by market and production context, but the underlying distinction is useful when evaluating a process.
Controlling oxidation and metal losses
Aluminium develops oxide films when exposed to oxygen. During charging, melting, transfer and surface disturbance, oxidation can contribute to metal losses and non-metallic residues.
Scrap size, surface condition, furnace operation, temperature control, handling practices and melt exposure all influence the outcome.
A practical process review should therefore measure metal recovery rather than relying only on how quickly the furnace melts the charge.
6. Fluxing, Dross Removal and Alloy Adjustment
After melting, the metal may require additional treatment to meet its target composition and cleanliness requirements.
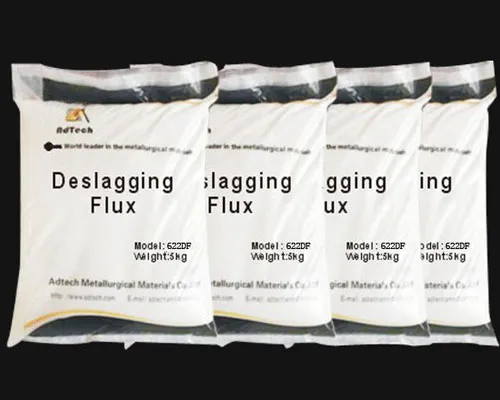
Fluxes are used in various aluminium recycling operations, but their function depends on the flux formulation and the process in which it is applied.
What does flux do in aluminium recycling?
Depending on the formulation and application, flux can help protect the melt surface, support separation of unwanted material, assist metal recovery from dross or perform a defined refining function.
It is not correct to assume that every flux removes the same contaminants or that fluxing alone can bring every melt to specification.
Common functional categories include:
| Flux category | Typical purpose | Key consideration |
|---|---|---|
| Covering flux | Helps protect the molten metal surface | Compatibility with the process and melt conditions |
| Refining flux | Supports specified melt-refining functions | Alloy, impurity type, treatment method and dosage |
| Deslagging or drossing flux | Assists separation of metal from surface residues | Dross characteristics and the recovery procedure |
| Furnace cleaning flux | Used to address suitable deposits on furnace surfaces | Furnace condition and the manufacturer’s operating instructions |
| Recycling flux | Used in selected processes to recover metallic aluminium from dross or ash | Residue composition and recovery equipment |
The International Aluminium Institute describes the use of salt fluxes in many scrap-refining processes to cover molten metal, help remove impurities and reduce oxidation. It also identifies dross, skimmings and salt slag as process residues requiring suitable handling and recovery routes. Not all recycling processes use the same flux system.
Removing dross
Dross forms as oxide-bearing material and other constituents accumulate at the molten metal surface. Depending on the process, some of this material contains recoverable aluminium.
Surface dross removal must be coordinated with the furnace and metal-handling procedure. Aggressive or poorly controlled handling can increase oxidation, while unsuitable residue treatment can lead to avoidable losses.
Dross should be managed as a recoverable process residue where technically and economically appropriate, with handling and final treatment selected for the actual material.
Alloy composition adjustment
After melting, producers may add suitable alloying materials or blend metal to achieve the required chemistry.
A representative chemical analysis is essential when the target specification is strict. The relevant elements depend on the grade and the final application.
Fluxing, skimming and alloy adjustment solve different problems. A well-designed process defines the purpose of each treatment rather than assuming one step can correct every type of impurity.
7. Melt Refining: Degassing and Filtration
For recycled aluminium intended for demanding casting applications, melt treatment may be necessary after melting and initial refining.
Two important operations are degassing and filtration. They are complementary, but they do not perform the same function.
Read more: How to Purify Aluminum: Degassing, Fluxing, Filtration, Methods.
7.1 Degassing removes dissolved hydrogen
Hydrogen can dissolve in molten aluminium and contribute to gas porosity when the metal solidifies under unsuitable conditions.
Industrial degassing commonly uses an inert gas such as argon or nitrogen introduced into the melt through a suitable treatment system. Hydrogen transfers from the melt into the gas bubbles and is carried away.
The effectiveness of degassing depends on parameters such as gas delivery, rotor or injector design where applicable, melt temperature, treatment time, alloy condition and initial hydrogen content.
A degassing system does not correct an incorrect alloy composition, and the presence of a degassing unit does not by itself guarantee a particular final hydrogen level. Appropriate operating conditions and verification are required.
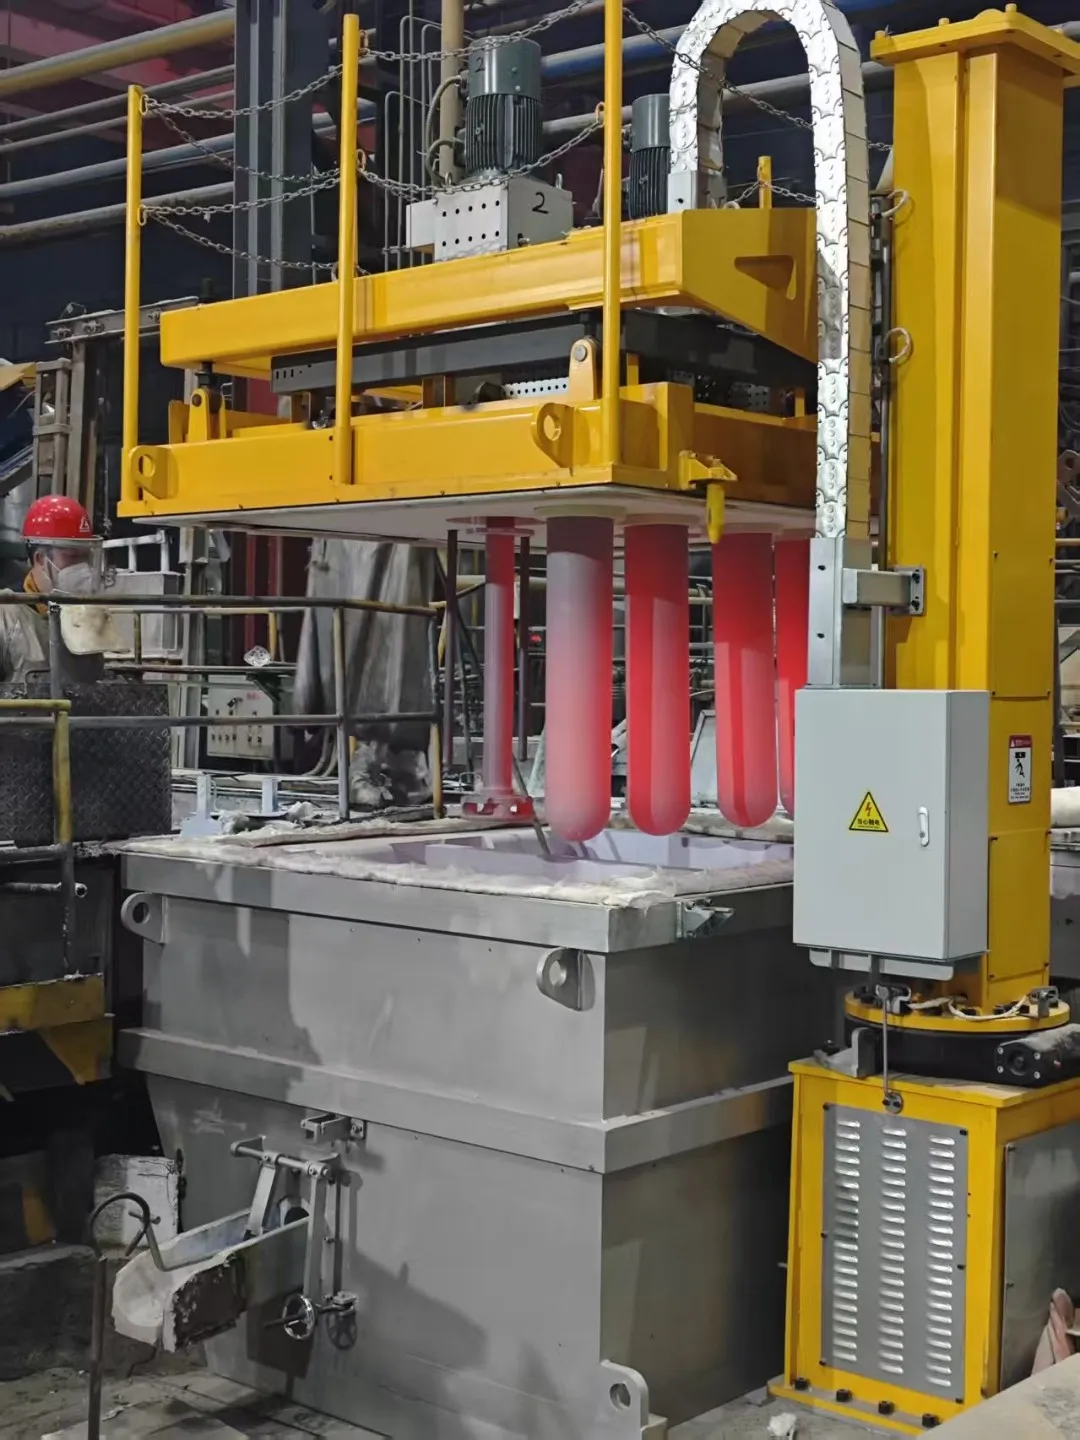
7.2 Filtration removes non-metallic inclusions
Molten aluminium may contain oxide films and other non-metallic inclusions. These can contribute to casting defects and reduce product quality.
Ceramic foam filters are used in suitable aluminium casting applications to capture or retain inclusions through a combination of filtration mechanisms and interactions with the filter structure.
The filter must be selected according to the required cleanliness, metal flow rate, alloy, filtration arrangement and casting conditions.
A filter that is too restrictive for the required flow may disrupt production, while an unsuitable filter arrangement may fail to deliver the desired cleanliness.
Degassing versus filtration
| Process | Main target | What it does not replace |
|---|---|---|
| Degassing | Dissolved hydrogen and other specifically targeted melt constituents, depending on process configuration | Alloy chemistry control and inclusion filtration |
| Ceramic foam filtration | Non-metallic inclusions in the molten metal | Dissolved hydrogen removal |
| Flux treatment | Specific surface protection, refining or residue-separation functions, depending on the flux | All other melt-treatment operations |
| Alloy adjustment | Chemical composition | Physical removal of all inclusions or dissolved gas |
This distinction is particularly important in a recycling plant that produces metal for high-quality casting. Hydrogen control and inclusion control should be evaluated separately.
7.3 Which filtration solution should a plant consider?
Different filtration arrangements can suit different production requirements.
-
Ceramic foam filters: Used in appropriate casting lines where inclusion removal is required.
-
Cartridge filtration systems: Considered when the process requires a specific filtration arrangement and performance level.
-
Deep-bed filtration systems: Evaluated for production lines and filtration duties suited to that configuration.
Selection should follow the actual production target rather than assuming that the most complex filtration system is always the best choice.
For plants producing high-value alloys, filtration must be integrated with melting, melt treatment, metal flow and casting. It cannot compensate for poor scrap sorting or an unacceptably contaminated feedstock.
8. Casting and Final Product Quality Control
Once the molten metal meets the required chemical composition and melt-quality conditions, it can be cast into a form suitable for downstream processing.
Typical forms include:
-
Ingots for storage, transport or subsequent remelting.
-
Billets for extrusion.
-
Slabs for rolling.
-
Cast shapes for applications that use those products directly.
-
Liquid metal supplied to a downstream manufacturing operation where appropriate.
The correct casting route depends on the intended product and the capabilities of the facility. Secondary aluminium is not a single universal product: different casting applications impose different chemistry, cleanliness and dimensional requirements.
Quality checks before release
Quality control should be defined around the product specification and process risks.
| Quality check | Why it matters |
|---|---|
| Chemical composition analysis | Confirms that the metal meets the specified alloy composition |
| Hydrogen measurement where relevant | Assesses melt condition for applications sensitive to gas porosity |
| Inclusion or cleanliness assessment | Checks whether melt treatment meets the required cleanliness criteria |
| Temperature verification | Supports controlled transfer and casting |
| Casting inspection | Identifies relevant surface, dimensional or internal quality problems |
| Process and batch records | Help trace results back to scrap sources and operating conditions |
The appropriate test method and acceptance limits depend on the alloy and product. A generic article should not assign one universal hydrogen limit, inclusion level or defect tolerance to all recycled aluminium.
Traceability also matters. When a defect occurs, records of scrap source, alloy composition, melt treatment, sampling and casting conditions help determine whether the cause originated in the feedstock, melting operation or downstream process.
9. How Energy-Efficient Is Aluminium Recycling?
Aluminium recycling is generally much less energy-intensive than producing primary aluminium from bauxite. However, a percentage should always be interpreted against its stated system boundary.
The International Aluminium Institute reports that, using 2019 global production data and the cited life-cycle inventory modelling, primary aluminium production required approximately 186 GJ of primary energy per tonne from mine to cast house, compared with 8.3 GJ per tonne for recycled aluminium. The resulting estimated energy saving was 95.5%.
The Aluminum Association likewise describes secondary aluminium production as approximately 95% more energy-efficient than primary production.
These are industry-level comparisons. They do not mean that every recycling plant will reduce its own energy consumption by exactly 95%. Actual performance depends on the scrap stream, pre-treatment requirements, furnace type, plant efficiency, residue recovery and accounting boundaries.
What affects the environmental performance of a recycling plant?
Scrap preparation: Removing unsuitable contaminants and preparing scrap correctly can improve processing, but preparation itself consumes energy and resources.
Furnace efficiency: Charging practice, furnace condition, heat transfer, holding time and temperature control influence energy demand.
Metal recovery: Preventing avoidable oxidation and recovering metallic aluminium from suitable residues can improve the usable output obtained from each tonne of feedstock.
Emissions management: Shredding, thermal treatment, coatings, fuel combustion and some flux-based processes may generate dust, organic emissions or other pollutants requiring suitable controls.
Residue management: Dross, skimmings and salt slag must be handled and treated according to their composition and applicable requirements.
The IAI identifies dust, organic compounds, fuel-related carbon dioxide emissions and, in certain salt-flux processes, additional emissions and salt slag as environmental considerations in scrap refining. Suitable furnace design, process optimization and emissions controls are therefore part of responsible recycling.
10. Common Problems in Aluminium Recycling and How to Address Them
The most useful process improvement is often to identify the cause of a problem before increasing treatment intensity or purchasing additional equipment.
| Observed problem | Potential causes to investigate | Appropriate direction |
|---|---|---|
| Final alloy does not meet specification | Mixed alloys, contaminated scrap, incorrect blending or insufficient chemical verification | Improve incoming scrap classification and establish a controlled composition-adjustment procedure |
| Excessive metal loss | Oxidation, unsuitable scrap preparation, handling practices or inefficient dross recovery | Review charge characteristics, melting practice and residue treatment |
| Gas porosity in cast products | Hydrogen, solidification conditions or other casting-related causes | Measure hydrogen where appropriate and review melt treatment and casting conditions |
| Inclusion-related defects | Oxide films, contaminated feedstock, poor handling or inadequate filtration | Identify inclusion sources and verify the effectiveness of melt cleanliness controls |
| High energy consumption | Excessive holding time, unsuitable feed preparation, inefficient furnace operation or unnecessary reheating | Review energy use across preparation, melting, holding and transfer |
| Unstable production rate | Furnace limitations, poor charge consistency, bottlenecks in treatment or downstream casting | Assess the entire process rather than one machine in isolation |
| Excessive dust or fumes | Scrap contaminants, shredding, coatings, thermal treatment or inadequate extraction | Identify the emission source and verify suitable collection and treatment systems |
A defect does not automatically mean the filtration system is inadequate. Likewise, a low metal recovery rate cannot necessarily be solved by changing flux.
Reliable improvement begins with identifying where the loss or defect originates, measuring the problem and matching the solution to the cause.
11. How to Select Aluminium Recycling Equipment
Equipment selection should begin with the actual production requirement.
Before requesting quotations, establish the following:
-
Feedstock: What types of aluminium scrap will be processed, and how consistent are their alloy composition and contamination levels?
-
Capacity: What are the required hourly and annual throughput, operating hours and batch sizes?
-
Target product: Will the plant produce foundry alloys, extrusion billets, rolling slabs or another product?
-
Quality requirements: Which alloy specifications, cleanliness criteria and final product tests are required?
-
Existing equipment: What furnace, holding furnace, degassing, filtration and casting systems are already installed?
-
Operating conditions: What are the existing temperature profile, metal flow, transfer distance and production constraints?
-
Environmental and safety requirements: What treatment is required for dust, coatings, residues and process emissions under the local rules?
These details help determine whether a plant needs better pre-treatment, upgraded melting capacity, more reliable composition control, additional melt treatment or improved casting arrangements.
Where do fluxes and molten aluminium purification equipment fit?
AdTech’s published product portfolio includes refining fluxes, flux injection systems, online degassing equipment, ceramic foam filters, other filtration equipment and integrated launder equipment for molten aluminium processing. These products relate to specific melt-treatment and casting stages, rather than replacing the collection, sorting and pre-treatment stages of recycling.
For example:
-
Flux selection should match the intended treatment function and the manufacturer’s operating instructions.
-
Flux injection equipment may be relevant where controlled and repeatable flux delivery is required.
-
Degassing equipment should be considered when hydrogen control is a defined process requirement.
-
Ceramic foam filters should be evaluated when non-metallic inclusion removal is required.
-
Launder equipment should be considered for controlled transfer of molten aluminium and temperature management in the relevant casting layout.
The right configuration depends on the plant’s process, alloy range, throughput and final quality targets. A supplier should be able to explain the function and limitations of each proposed system, not simply provide a list of machines.
12. Frequently Asked Questions
Does every aluminium scrap type use the same recycling process?
No. Clean production scrap may require minimal preparation, while mixed scrap, coated products and machining turnings may need additional sorting, cleaning, drying or decoating. The route should reflect both the feedstock and the target product.
Can a ceramic foam filter remove hydrogen from molten aluminium?
No. A ceramic foam filter is designed to remove non-metallic inclusions. Dissolved hydrogen generally requires a suitable degassing process when hydrogen reduction is necessary.
Can aluminium recycling recover every kilogram of metal?
No. Metal losses can occur through oxidation, residues, handling and other process inefficiencies. Proper preparation, controlled melting and suitable residue recovery can improve metal yield, but a universal recovery rate would not be appropriate for all scrap types and plants.
How are painted aluminium cans prepared for recycling?
Depending on the coating and process requirements, used cans may be sorted, shredded or otherwise sized, and thermally treated to remove coatings before remelting. The specific treatment depends on the feedstock, equipment and emissions-control requirements.
What temperature is needed to melt aluminium scrap?
Pure aluminium melts at approximately 660°C, but actual furnace operating temperatures depend on alloy composition, furnace design and the requirements of the melting and casting process. The melting point should not be used as a universal operating setpoint.
Why is dross produced during aluminium melting?
Aluminium oxidation and the interaction of the melt with process residues contribute to dross formation. Dross may contain recoverable metallic aluminium, so appropriate handling and recovery methods can help reduce avoidable metal losses.
What are the main environmental concerns in aluminium recycling?
Key considerations include energy use, fuel-related emissions, dust from material handling, emissions associated with coatings and thermal treatment, and the management of dross or salt slag. The actual impact depends on the process route, input scrap and emissions controls.
Conclusion
The aluminium recycling process is a coordinated sequence of material preparation, melting, metal refining and casting. Its performance depends on the condition and composition of the scrap, safe charging practices, appropriate furnace operation and effective control of the final metal quality.
For industrial producers, the most important principle is to match each treatment to a defined problem. Sorting controls feedstock consistency, fluxing supports specific refining and residue-separation functions, degassing addresses dissolved hydrogen, and filtration targets non-metallic inclusions. When these operations are selected and controlled together, a recycling plant is better positioned to achieve consistent metal quality, efficient metal recovery and responsible resource use.